Ultimate Buyer’s Guide: Who is the Best Manufacturer for Pallet Racks for Your Warehouse?
If you're in the market for warehouse pallet racking, you aren't just buying equipment. You're making a strategic choice that dictates your operational flow, worker safety, scalability, and long-term overhead.
The right storage system accelerates inventory turnover and ensures load stability while minimizing workplace hazards. On the flip side, partnering with the wrong manufacturer often leads to structural failures, installation headaches, missed deadlines, and serious safety risks.
Here is the hard truth:
There is no single "best" manufacturer for everyone.
The right choice depends on your specific facility layout, budget, geographical location, inventory profile, and required lead times.
Instead of just ranking brands, this guide is designed to help you identify which partner actually fits your project goals.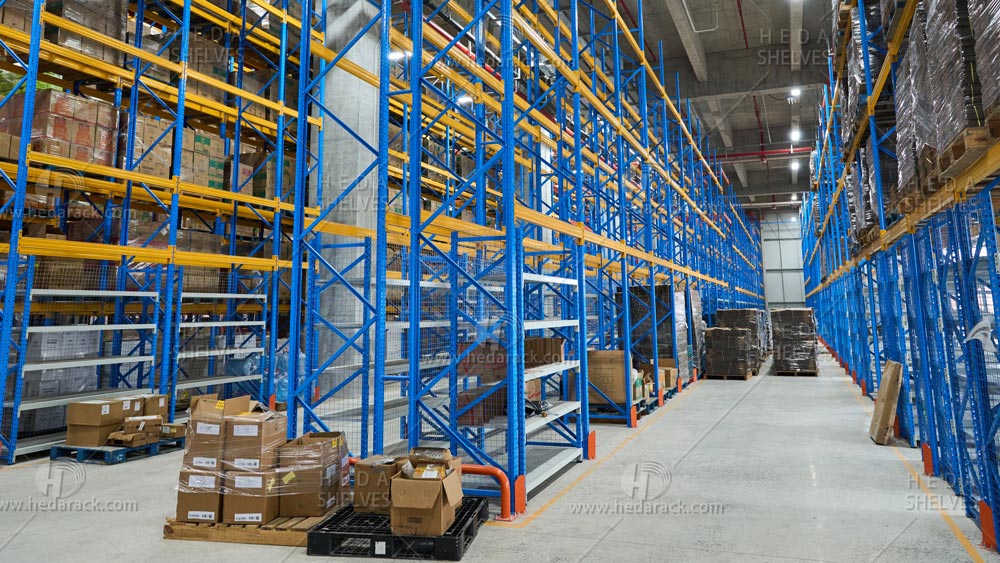
What Defines a Top-Tier Pallet Rack Manufacturer?
Before comparing names, you need a solid framework for evaluation. A professional choice isn't based on marketing volume, but on a supplier's ability to provide consistent, compliant, and durable solutions.
Adherence to Industry Safety Standards (RMI & ANSI)
Safety is the non-negotiable starting point.
A reputable manufacturer prioritizes engineering codes. In North America, RMI and ANSI standards are the gold standard for design, manufacturing, and usage protocols. For a buyer, these certifications ensure that your racking isn't just "good enough"—it's backed by rigorous structural calculations and load testing.
Key questions to ask:
- Can the supplier provide detailed structural design specifications?
- Are load capacities, blueprints, and testing data readily available?
- Do they follow strict material and process controls required by your local market?
- Do they support third-party safety audits for large-scale projects?
If a manufacturer is vague about these technical fundamentals, it's a major red flag.
Material Integrity: Structural vs. Roll-Formed Steel
Next, look at the physical construction. Pallet racks generally fall into two categories: structural steel and roll-formed steel. Neither is "better" in a vacuum; they serve different purposes.
Structural steel racking is heavy-duty and robust. It’s built for high-impact environments where forklifts are constantly on the move and loads are extremely heavy. Its primary advantage is sheer durability and resistance to damage in demanding conditions.
Roll-formed steel is the go-to for standard warehousing. It is lighter, more versatile, and easier to mass-produce, which usually means faster delivery. For most general storage needs, roll-formed racking offers the best balance of performance and cost-efficiency.
Think of it this way:
- Structural Steel = Industrial-strength durability for heavy loads.
- Roll-Formed = Standardized efficiency and cost advantages.
A quality manufacturer won't just push one product; they will recommend the type that matches your specific operational environment.
Engineering Expertise and Customization
A great manufacturer does more than just "take an order and ship it." You need a partner who understands warehouse dynamics—someone who can design a system tailored to your pallet sizes, forklift aisles, fire safety codes, and floor conditions.
Professional manufacturers typically provide:
- Strategic warehouse floor plan consultations.
- Comparative analysis of different racking configurations.
- Precise load-bearing and span calculations.
- Custom sizing for unique inventory needs.
- On-site installation guidance and support.
This engineering phase is critical. Most project failures happen because of poor initial planning, not because of the steel itself.
Evaluating Industry Leaders: Finding Your Best Match
While the market is diverse, several key players have established themselves as industry benchmarks. Each excels in a specific area.
Use the following comparison to help narrow down your search:
Frazier Industrial Company: The Structural Steel Specialists
If your warehouse demands maximum strength, Frazier is a name that often comes up. They are known for their deep expertise in structural steel, making their systems ideal for heavy-duty applications where racks are prone to forklift impacts.
Their value proposition centers on:
- Rugged structural integrity.
- Superior impact resistance.
- Stability under heavy loads and high-frequency cycles.
If your environment is "tough" on equipment, this type of manufacturer should be at the top of your list.
Ridgurak: Innovation Paired with Availability
For projects where speed and inventory depth are the primary concerns, manufacturers like Ridgurak stand out. They have built a reputation for having the stock levels needed to respond quickly to large orders.
Their competitive edge includes:
- Massive ready-to-ship inventory.
- A wide variety of product options.
- Faster lead times for standard components.
When you need to scale up quickly or handle a sudden expansion, delivery speed often outweighs custom engineering.
Speedrack: The Standard for Roll-Formed Efficiency
For standard storage and distribution centers, Speedrack is a prominent choice for roll-formed solutions. They focus on high-quality, standardized products that fit a wide range of common warehouse needs.
Key benefits include:
- Consistent manufacturing quality.
- Competitive pricing through standardization.
- Perfect fit for standard pallet dimensions.
This is often the most practical choice for general logistics hubs and medium-duty industrial storage.
Global Options: Why International Brands like HEDA or Maxrac are Gaining Traction
In recent years, global manufacturers have become increasingly popular, especially those who can bridge the gap between competitive pricing and professional engineering support.
Brands like HEDA and Maxrac compete on three main fronts:
- Highly competitive factory pricing.
- Greater flexibility for custom modifications.
- Direct project-level responsiveness.
This model is attractive because it offers more than just a low price tag; it provides a collaborative partnership that scales with the project's complexity.
Choosing Based on Your Specific Operational Needs
Now that you know the players, let's look at your specific requirements.
Best for Heavy-Duty and High-Impact Settings
If your facility handles heavy materials, uses forklifts constantly, and operates in a high-traffic environment, structural steel is your best bet. It offers the longevity and safety margin needed for industrial manufacturing and raw material storage.
Best for High-Density Storage (VNA, Drive-in, Radio Shuttle)
When the goal is to maximize every square inch of floor space, you need high-density systems like:
These projects require more than just steel; they require system integration. You need a manufacturer capable of coordinating the racking with your specific vehicles, pallets, and workflow.
Best for Fast Deployment and Budget-Sensitive Projects
For growing businesses or tight timelines, the priorities shift to:
- Lead times.
- Total landed cost.
- Ease of installation.
In these scenarios, standardized roll-formed products or global manufacturers with fast production cycles offer the best path forward.
Why HEDA is a Strong Candidate for Your Next Project
If you are currently vetting suppliers, HEDA brings a unique balance of safety, value, and technical support to the table. We don't claim to be the only "best" choice, but we are often the right choice for businesses looking for a reliable, factory-direct partner.
Our Focus on Safety and Global Compliance
Safety isn't an "extra"—it's the foundation of every rack we build. HEDA emphasizes structural stability and rigorous load calculations to ensure your facility remains compliant and your team stays safe over the long term.
Factory-Direct Value Without Quality Trade-offs
Working directly with HEDA means cutting out the middleman. This factory-direct model provides:
- Transparent pricing.
- A shorter, more accurate communication chain.
- Faster response times for custom adjustments.
We prove that competitive pricing can go hand-in-hand with high manufacturing standards.
Full Project Lifecycle Support: Design to Installation
We don't just sell components; we deliver operational systems. HEDA provides comprehensive support, from initial CAD layout designs to final installation guidance. This end-to-end approach reduces the logistical burden on your team and minimizes the risk of costly onsite errors.
Common Mistakes to Avoid During Your Selection Process
Choosing a manufacturer isn't just about picking the lowest quote. Avoid these common pitfalls:
Ignoring Lead Times and Total Shipping Costs
A low unit price can quickly be erased by long wait times or exorbitant freight costs. Always confirm:
- The actual production timeline.
- Shipping logistics and container optimization.
- Local port fees and destination charges.
A "cheap" rack that arrives three months late is rarely a bargain.
Overlooking Local Seismic and Building Codes
Your racking system must respect the laws of physics—and the local laws of your city. Seismic requirements, anchoring standards, and fire safety clearances vary by region. If your manufacturer doesn't understand these local nuances, your project is at risk.
Conclusion: Finalizing Your Decision
So, who is the best pallet rack manufacturer?
The answer is simple: The one that fits your specific operational goals.
- For maximum durability: Look at structural specialists.
- For space optimization: Look for system integrators.
- For ROI and speed: Look at factory-direct global manufacturers.
Don't just buy a brand name. Define your needs clearly, and choose a partner who views your warehouse efficiency as their own success.
If you’re planning a new facility or upgrading your current storage, reach out for a professional consultation. Starting with the right advice is the fastest way to a successful warehouse.